
The best MIG welding wire depends first on the metal you are joining. Mild steel needs a compatible steel filler, while aluminum needs the right aluminum alloy and feeding setup.
For general mild-steel work, INEFIL ER70S-6 is our top pick because its ER70S-6 classification supports single- and multi-pass welding across common construction jobs. YESWELDER ER70S-6 is the value pick for everyday steel repairs.
We checked exact model specifications, current product availability, base-metal compatibility, spool size, shielding-gas guidance, and recall records before rebuilding these picks.
Best MIG Welding Wire Compared
| Product | Best for | Material | Spool weight | Wire diameter | Score |
|---|---|---|---|---|---|
|
Mid-range
|
All-position mild steel | Carbon/C-Mn steel | 10 lb | .030 in | 92/100 |
|
Premium
|
Mill scale and production | Mild steel | 12.5 lb | .030 in | 90/100 |
|
Budget
|
General steel repairs | Mild/carbon steel | 10 lb | .030 in | 88/100 |
|
Budget
|
5000-series aluminum | Aluminum | 1 lb | .030 in | 87/100 |
|
Mid-range
|
General fabrication | Mild steel | 11 lb | .030 in | 80/100 |
Best MIG Welding Wire: Our Top Picks
1. INEFIL ER70S-6
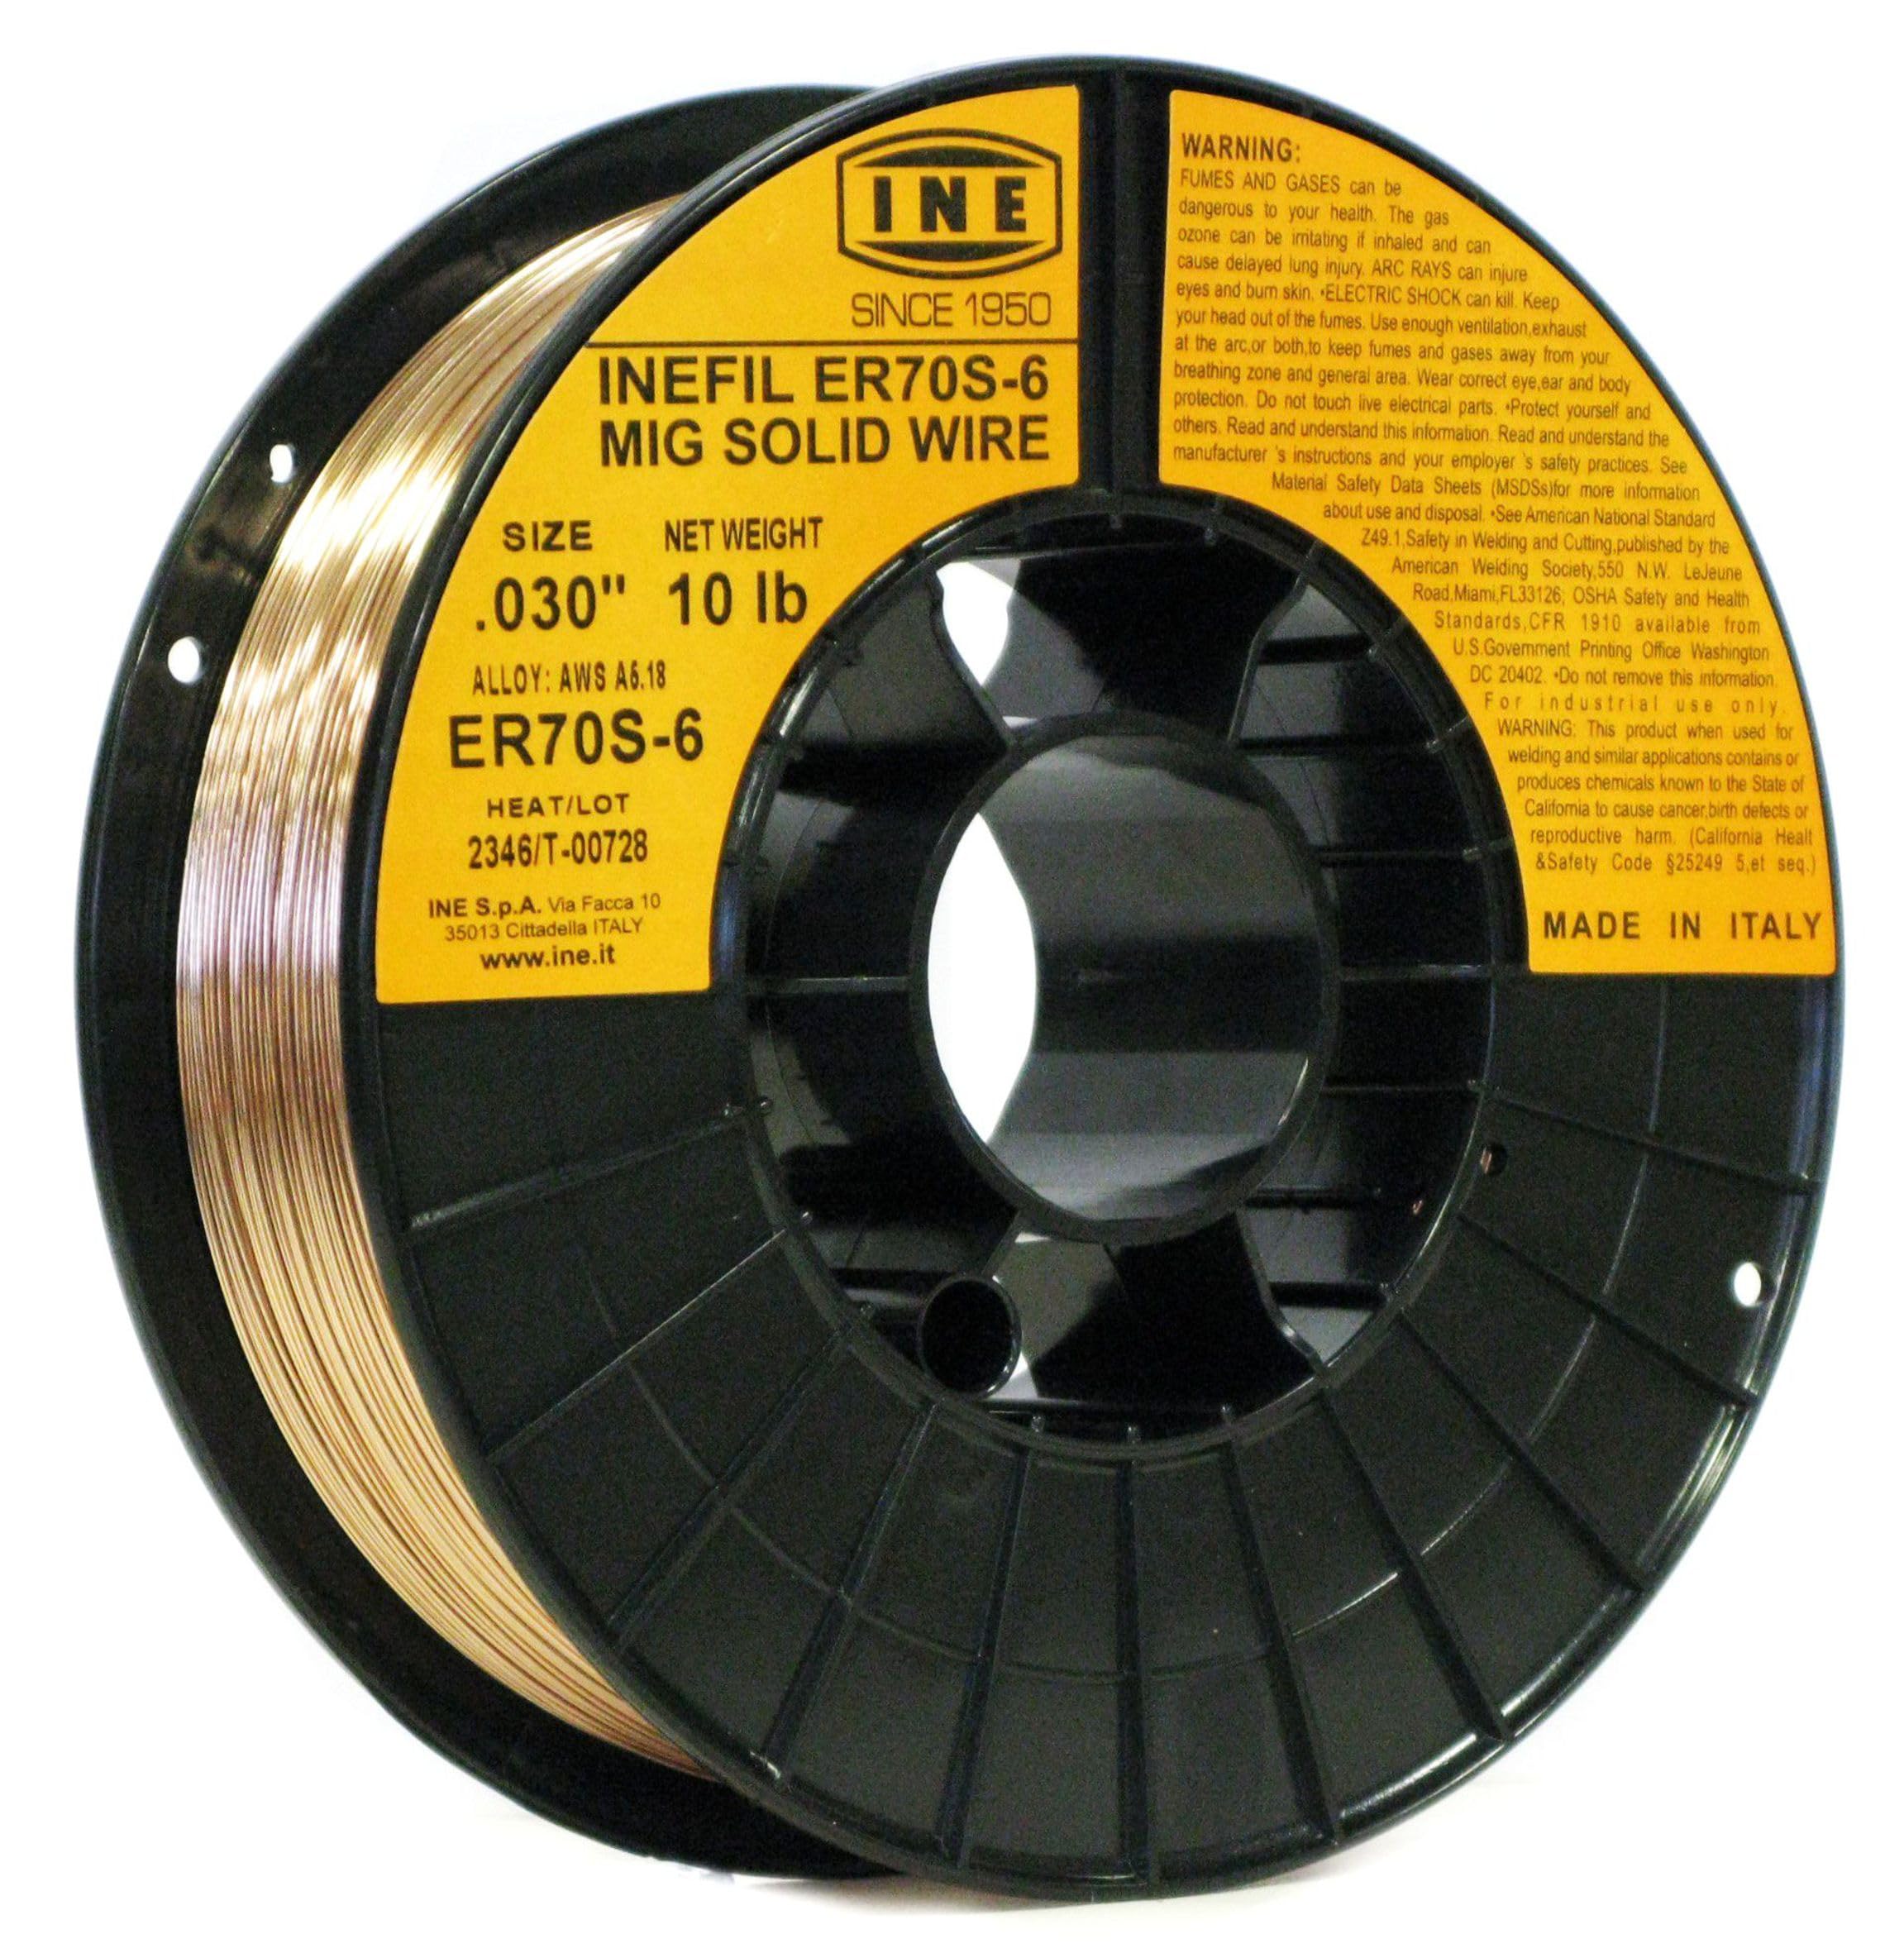
Bottom line: INEFIL ER70S-6 is the most versatile steel pick here if you want one .030-inch ER70S-6 wire for general construction, repair, and multi-pass work.
- Classification: AWS ER70S-6, a common solid steel MIG filler
- Material: Carbon and C-Mn steel, for general steel fabrication
- Wire diameter: .030 in, fits many hobby and shop MIG setups
- Spool weight: 10 lb, suited to longer shop sessions
- Shielding gas: Ar/CO2 or CO2, giving common shop gas options
INE classifies this wire as ER70S-6 for carbon and carbon-manganese steels. The manufacturer lists it for single- and multi-pass welding, including structural work, tanks, boilers, and construction.
The important correction is strength wording: the wire is intended for steels up to 510 MPa tensile strength. That is not the same as saying the wire itself has a fixed 510 MPa tensile rating.
- ER70S-6 classification suits a broad range of mild-steel work
- Supports single- and multi-pass welding
- Works with common Ar/CO2 blends or CO2
- 10 lb spool reduces changeovers during longer projects
- Not intended for aluminum or stainless-steel jobs
- A 10 lb spool may not fit compact welders
- Surface preparation is still important for sound welds
2. Lincoln SuperArc L-56

Bottom line: Lincoln SuperArc L-56 is the premium steel option for production work, mill scale, and shops that want Lincoln’s documented feeding and all-position specifications.
- Classification: AWS ER70S-6, designed for mild-steel GMAW
- Material: Mild steel, with higher Mn/Si deoxidizers
- Wire diameter: .030 in, a common shop size
- Spool weight: 12.5 lb, gives longer run time between changes
- Shielding gas: CO2 or argon-rich mixes, broad process flexibility
Lincoln lists SuperArc L-56 for sheet metal, automotive work, structural steel, robotic welding, and applications with medium to heavy mill scale. Its higher manganese and silicon content is designed to improve deoxidation and bead wetting.
The .030-inch variant is documented on a 12.5 lb plastic spool. Lincoln also rates L-56 for all welding positions and lists 100% CO2 plus common argon/CO2 or argon/O2 shielding options.
- Official ER70S-6 classification for mild steel
- Documented for all welding positions
- Designed to tolerate medium to heavy mill scale
- 12.5 lb spool suits frequent shop use
- Larger spool may not fit smaller machines
- Premium positioning is unnecessary for occasional light repairs
- Not a filler for aluminum jobs
3. YESWELDER ER70S-6

Bottom line: YESWELDER ER70S-6 is the value-focused choice for routine mild-steel repairs and fabrication when you still want a 10 lb ER70S-6 spool.
- Classification: ER70S-6, for solid-wire steel MIG welding
- Material: Mild, carbon, and low-alloy steel
- Wire diameter: .030 in, common for general repair work
- Spool weight: 10 lb, reduces frequent spool changes
- Shielding gas: CO2 or Ar/CO2, compatible with common shop gases
YESWELDER lists this copper-coated ER70S-6 wire for mild, carbon, and low-alloy steel. Its manganese and silicon content is intended to help when steel has mill scale, rust, or light surface contamination.
It fits common repair, automotive, farm-equipment, and general fabrication jobs. As with any solid MIG wire, correct drive-roll tension, a clean liner, and the machine’s starting chart matter more than brand alone.
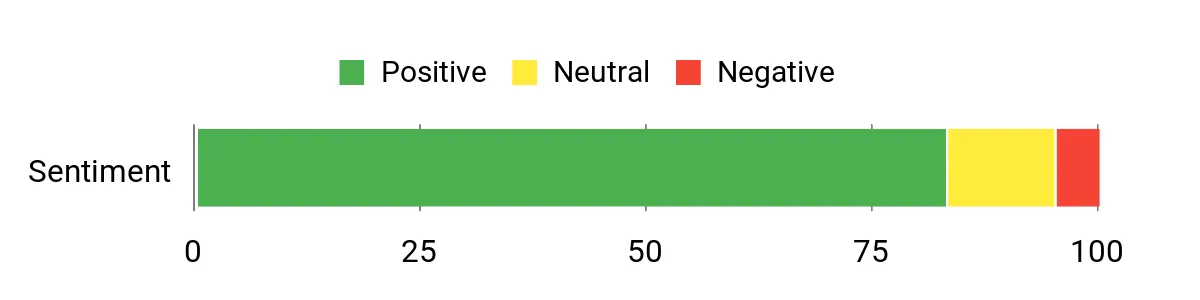
- 10 lb spool for longer repair and fabrication sessions
- ER70S-6 chemistry supports common mild-steel work
- Compatible with CO2 or Ar/CO2 shielding gas
- Copper-coated wire is designed for predictable feeding
- Not suitable for aluminum welding
- Still requires shielding gas
- Dirty steel should be cleaned when practical
4. Hobart ER5356

Bottom line: Hobart ER5356 is the specialist pick for 5000-series aluminum when you need .030-inch ER5356 wire and corrosion resistance for exposed aluminum work.
- Classification: ER5356, an aluminum filler alloy
- Material: Aluminum, intended for 5000-series base metals
- Wire diameter: .030 in, suited to compatible aluminum MIG setups
- Spool weight: 1 lb, convenient for occasional aluminum jobs
- Shielding gas: 100% argon, the recommended setup for this wire
Hobart identifies ER5356 as a general-purpose aluminum filler with relatively high shear strength and excellent saltwater corrosion resistance. The .030-inch product is supplied on a 1 lb spool.
This wire is not an alternative to ER70S-6 steel wire. Aluminum is softer and needs a compatible feed path; many MIG machines use a spool gun or another aluminum-capable system to avoid feeding problems.
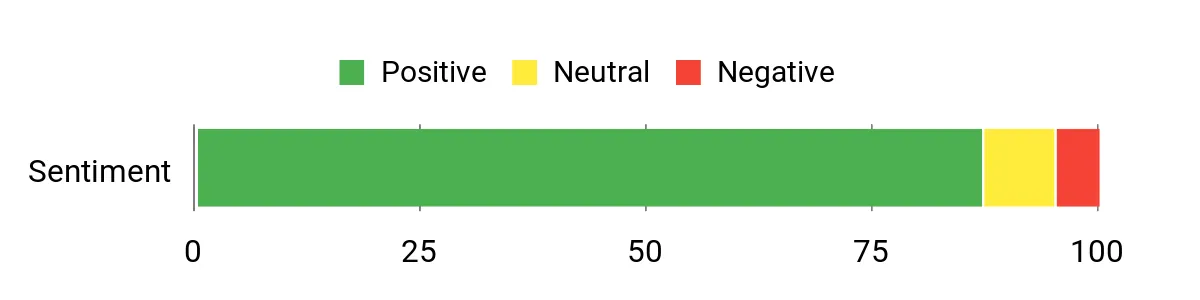
- Correct alloy family for many 5000-series aluminum jobs
- Excellent saltwater corrosion resistance
- Compact 1 lb spool is practical for occasional use
- Official Hobart identification confirms the .030-inch ER5356 variant
- Not suitable for steel
- Requires shielding gas
- Aluminum feeding may need a spool gun or other compatible setup
5. Harris E70S6

Bottom line: Harris E70S6 is a practical fabrication pick when you want an 11 lb .030-inch ER70S-6 spool with strong deoxidizer content for ordinary mild-steel shop work.
- Classification: AWS A5.18 ER70S-6, general-purpose steel filler
- Material: Mild steel, for fabrication and repair
- Wire diameter: .030 in, a common solid-wire size
- Spool weight: 11 lb, suited to repeated shop work
- Shielding gas: CO2 or argon/CO2 mixes, common GMAW choices
Current Harris distributor specifications identify model E70S6E5 as .030-inch ER70S-6 mild-steel MIG wire on an 11 lb spool. Harris describes the alloy as having a high silicon-and-manganese deoxidizer combination for better wetting.
The wire is listed for general fabrication, out-of-position short-circuit transfer, and multi-pass work where surfaces may retain rust or contamination. Cleaning the joint when practical still gives you a more predictable weld.
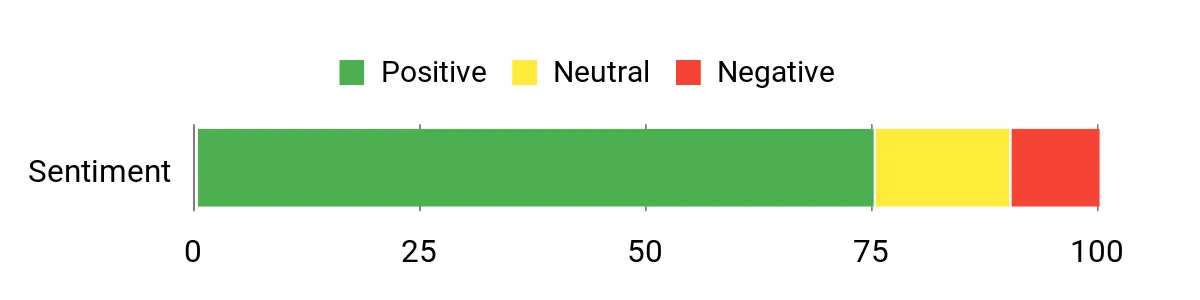
- AWS ER70S-6 classification for mild steel
- 11 lb spool supports longer fabrication sessions
- Additional deoxidizers improve tolerance of surface contamination
- Can run with CO2 or common argon/CO2 blends
- Not intended for aluminum
- An 11 lb spool may not fit compact welders
- Surface contamination should still be removed when practical
INEFIL ER70S-6 vs YESWELDER ER70S-6: Is the Upgrade Worth It?
Both are .030-inch, 10 lb ER70S-6 steel wires, so the practical difference is less about basic classification and more about documented applications, brand positioning, and your budget.
- Classification: Both are ER70S-6 solid wires for common steel MIG work.
- Spool format: Both linked variants are .030-inch wire on 10 lb spools.
- Documentation: INE publishes broader industrial approvals and construction-use data; YESWELDER emphasizes everyday fabrication and repair.
- Value: YESWELDER is the lower-priced choice based on the current listings checked privately.
Which MIG Welding Wire Should You Buy?
- One versatile steel spool: get the INEFIL ER70S-6.
- Mill scale or production work: get the Lincoln SuperArc L-56.
- Value-focused steel repairs: get the YESWELDER ER70S-6.
- 5000-series aluminum: get the Hobart ER5356.
- General fabrication with strong deoxidizer content: get the Harris E70S6.
How We Chose
- Base-metal match: We prioritized the correct AWS filler classification for steel or aluminum.
- Exact variant: We checked wire diameter, spool weight, and model identifiers against primary or current product sources.
- Process fit: We checked shielding-gas guidance, feeding needs, and documented welding positions or applications.
- Availability and safety: We checked current listings and searched recall records for the exact product families.
- Owner feedback: We only use trend claims when multiple independent non-Amazon sources support the same pattern.
Customer Preferences
Choose by compatibility before brand. The three ER70S-6 steel options target overlapping mild-steel work, while Hobart ER5356 serves a different aluminum use case. Spool fit, wire diameter, gas, and base-metal alloy should decide the shortlist.
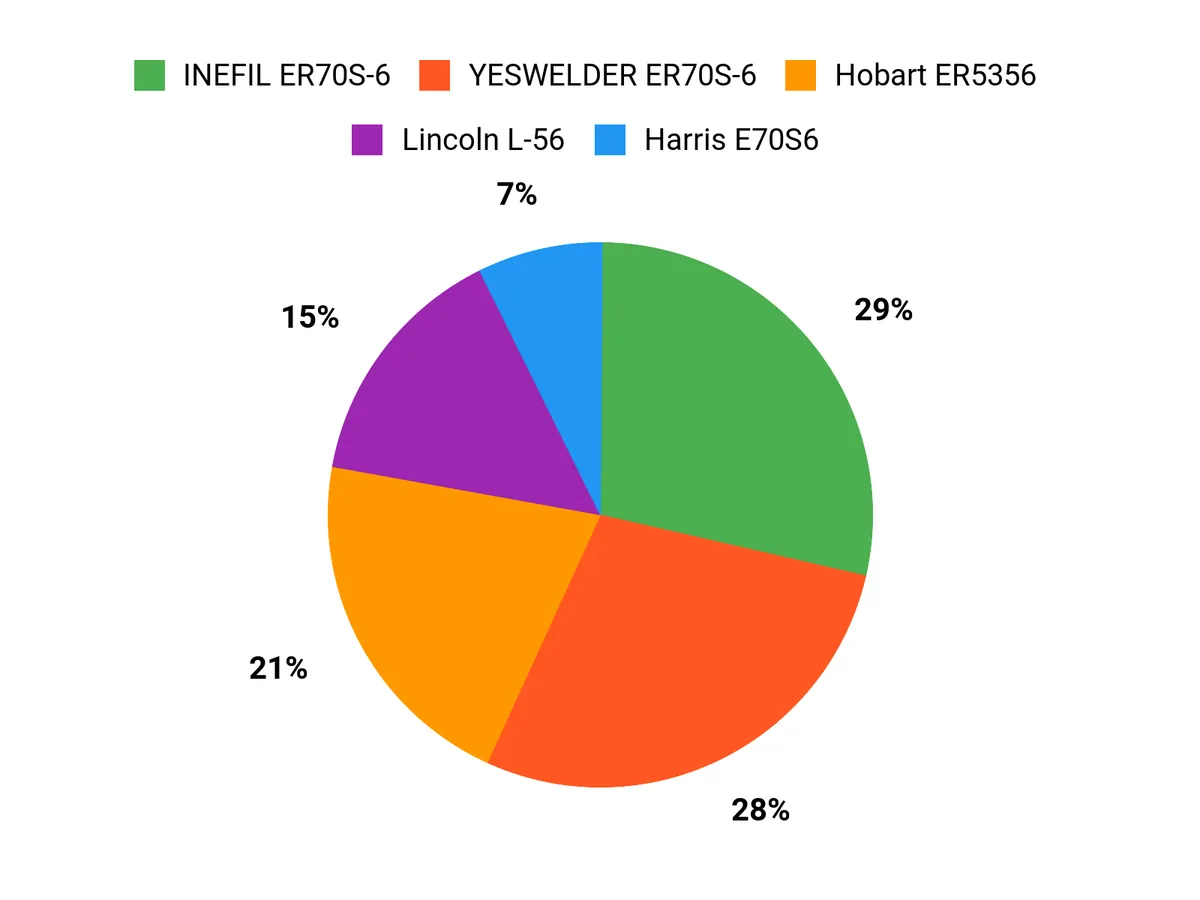
MIG Welding Wire Buying Guide
Match the Wire to the Base Metal
Start with the metal, not the brand. ER70S-6 is for common carbon and mild steels, while ER5356 is an aluminum filler used with many 5000-series alloys. For general steel work, INEFIL ER70S-6 is the broadest fit in this group.
Choose a Diameter Your Welder Supports
Every linked pick here uses .030-inch wire, but that does not make .030 right for every job. Your welder’s door chart or manual should match wire diameter to material thickness, voltage, and wire-feed speed. Use the specified drive-roll groove and contact tip.
Check Spool Size Before You Order
Spool weight affects machine fit and how often you stop to change wire. Compact welders may accept only smaller spools, while shop machines often take larger ones. Check hub size and maximum spool capacity before buying a 10, 11, or 12.5 lb spool.
Use the Correct Shielding Gas
The ER70S-6 steel wires here can run with CO2 or suitable argon-based mixtures according to their manufacturers. Hobart ER5356 is aluminum wire and should use the aluminum setup recommended by the welder maker; 100% argon is the documented recommendation for this Hobart wire.
Think About Surface Condition
ER70S-6 uses manganese and silicon deoxidizers, which improve tolerance of mill scale and light contamination. Lincoln SuperArc L-56 is specifically documented for medium to heavy mill scale. Even so, removing rust, oil, paint, and moisture remains the safer path to consistent weld quality.
Plan the Feed Path for Aluminum
Aluminum wire is softer than steel wire and is more prone to feeding trouble through a long standard liner. Many MIG systems use a spool gun or another aluminum-capable feed system. Follow the welder manual for drive rolls, liner, polarity, gas, and starting parameters.
Mistakes to Avoid When Buying MIG Welding Wire
- Buying by diameter alone: confirm the filler classification and base-metal alloy first.
- Ignoring spool capacity: verify the welder can physically accept the spool.
- Using the wrong gas: follow the wire and welder manufacturer’s process guidance.
- Overtightening the feed system: use enough tension to feed without crushing or deforming wire.
- Skipping test beads: start from the machine chart and fine-tune on scrap before the final joint.
FAQs
Which MIG Welding Wire Should I Choose?
Match the wire to the base metal first. ER70S-6 is a common solid-wire choice for mild and carbon steel, while ER5356 is for compatible aluminum alloys, especially many 5000-series materials. Then confirm diameter, spool size, shielding gas, and welding position against your welder manual and the filler manufacturer’s data.
How Do I Fix Feeding and Tangling Issues?
Check spool orientation, hub tension, drive-roll groove, drive-roll pressure, liner condition, and contact-tip size. Too much tension can deform wire or create a bird’s nest, while a dirty or worn liner adds drag. Make sure the spool is seated correctly, then feed wire with the gun as straight as practical while testing.
What Gas and Settings Should I Use?
For the ER70S-6 steel wires here, manufacturers allow CO2 or suitable argon-based mixtures, depending on the wire and transfer mode. For Hobart ER5356 aluminum wire, 100% argon is the documented recommendation. Start with your welder’s chart for the chosen wire diameter and material thickness, then make short test beads before welding the part.
Is ER70S-6 Good for Dirty or Rusty Steel?
ER70S-6 has relatively high manganese and silicon deoxidizer content, so it handles mill scale and light surface contamination better than some lower-deoxidizer solid wires. That does not make surface preparation optional. Remove oil, paint, moisture, heavy rust, and loose scale whenever possible, especially for structural or safety-critical work.
Can I Use Steel MIG Wire for Aluminum?
No. Steel filler such as ER70S-6 is not a substitute for an aluminum filler. Aluminum welding requires a compatible filler alloy, shielding gas, and feed setup. For many 5000-series aluminum jobs, ER5356 is a common choice, but the exact filler should match the base alloy and service requirements.
Is .030 or .035 MIG Wire Better?
Neither diameter is universally better. The right size depends on your machine, material thickness, transfer mode, and amperage range. All five linked products in this roundup are .030-inch variants, which makes them easy to compare, but you should still follow your welder’s chart instead of switching diameters based on a general rule.
Final Verdict
For the best MIG welding wire across common mild-steel jobs, INEFIL ER70S-6 stands out for its documented ER70S-6 classification, single- and multi-pass use, and broad construction applications. Your base metal and machine compatibility should still come first.
For lower-cost general steel work, see YESWELDER ER70S-6. For a premium production-focused steel option, see Lincoln SuperArc L-56.
| Product Name | Image | Rating | Material | Spool Weight | Wire Diameter |
|---|---|---|---|---|---|
| INEFIL ER70S-6 MIG Welding Wire .030″ — 10 lb Spool |
|
4.7/5 (2,193 reviews) | Carbon Steel | 10 lb | .030 inches |
| Lincoln Electric MIG Welding Wire, L-56, .030, Spool |
|
4.7/5 (143 reviews) | Alloy Steel | 12.5 lb | .030 inches |
| YESWELDER MIG Welding Wire, ER70S-6 Solid Carbon Steel 10LB .030″ |
|
4.7/5 (2,069 reviews) | Carbon Steel | 10 lb | .030 inches |
| Hobart ER5356 Aluminum MIG Welding Wire 0.030 in, 1 lb Spool |
|
4.7/5 (529 reviews) | Aluminum | 1 lb | .030 inches |
| Harris E70S6E5 ER70S-6 MS Spool with Welding Wire, 0.030 lb. x 11 lb. |
|
4.0/5 (N/A reviews) | Mild Steel | 11 lb | .030 inches |
[…] not transfer settings directly between them. If you are comparing consumable types, this guide to quality welding wire covers a separate wire […]
[…] a properly alloyed stainless-to-carbon-steel weld. If you are comparing wire types, this guide to MIG welding wire options is useful, but select a 309L-type stainless wire for the common dissimilar joint rather than […]
[…] and is widely applied in heavier fabrication where moderate contamination may exist. This all-position formulation enhances versatility, making it a popular choice among welders in various […]
[…] with different heat input and shielding requirements. If you are researching those systems, wire feed speed is one variable that must match the selected process rather than being copied from oxy-fuel brazing […]