Magnesium brazing can produce lightweight, metallurgical joints without melting the entire base part, but it demands much tighter control than ordinary steel or copper brazing. Magnesium forms a stubborn oxide film, has a relatively low melting temperature, and can burn intensely if overheated. Successful work depends on matching the magnesium alloy, brazing filler metal, flux, joint design, and heating cycle.
Quick Answer
Magnesium brazing normally uses a magnesium-compatible filler such as BMg-1/AZ92A with a dedicated chloride-fluoride flux. For BMg-1, brazing is commonly performed around 1120°F to 1160°F (605°C to 627°C), not 1200°F to 1400°F. Clean surfaces, controlled heating, complete flux removal, ventilation, and Class D fire protection are essential.
Key Takeaways
- BMg-1, also associated with AZ92A composition, is a recognized magnesium brazing filler; filler choice must still match the specific base alloy.
- Magnesium needs dedicated flux chemistry because its oxide film strongly resists normal brazing conditions.
- Brazing temperature must stay below the base alloy’s solidus; overheating can melt or ignite the workpiece.
- Flux residue should be removed thoroughly because many magnesium brazing fluxes are corrosive and hygroscopic.
- Magnesium chips, dust, or burning metal require appropriate Class D fire protection rather than an ordinary multipurpose extinguisher.
What Is Magnesium Brazing?
)
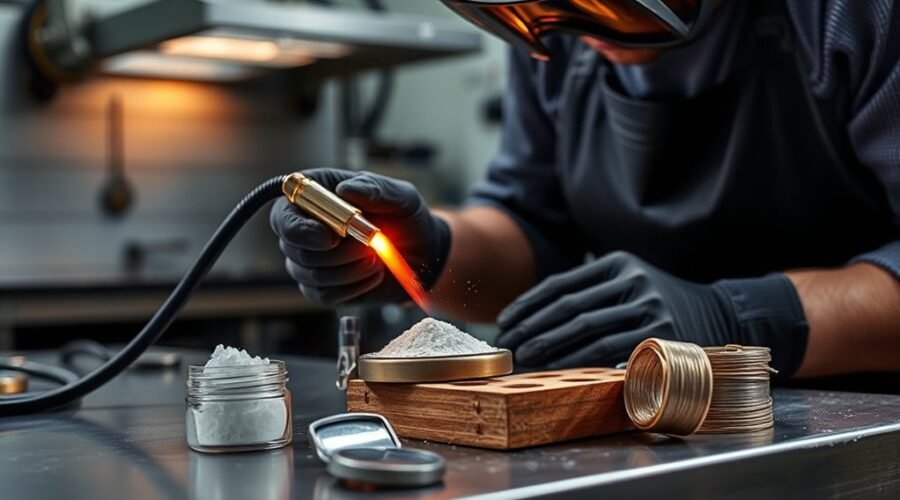
Magnesium brazing joins compatible magnesium parts by melting a filler metal that flows between closely fitted surfaces while the base metal remains solid. The American Welding Society’s magnesium-alloy brazing guidance covers torch, furnace, and dip brazing as established processes.
The main difficulty is the surface film. Magnesium readily forms magnesium oxide and related surface compounds that interfere with wetting, so clean metal alone is not enough. The joint must remain protected from renewed oxidation while the filler becomes fluid.
Flux performs that job in conventional magnesium brazing. It disrupts or dissolves the oxide layer and helps the molten filler wet the joint faces and move through the clearance by capillary action.
Heat also changes the base material. Brazing can soften work-hardened magnesium alloys, especially when an entire assembly is heated in a furnace or salt bath. Torch brazing concentrates heat in a smaller area, but temperature control remains critical.
Is Magnesium Brazing Safe?
Magnesium brazing can be performed safely only with proper hot-work controls. The main hazards are ignition of magnesium, hot flux, irritating fumes, molten filler, and fine magnesium chips or dust left near the work area.
Warning: Do not treat a magnesium fire like an ordinary wood or paper fire. Combustible magnesium, especially chips, flakes, or powder, requires an extinguishing agent specifically approved for the relevant Class D metal fire.
OSHA identifies magnesium as a Class D combustible-metal hazard and specifies special extinguishers for fires involving magnesium powders, flakes, or shavings. Ordinary ABC extinguishers are not automatically suitable for burning magnesium.
Ventilation is equally important. OSHA’s welding, cutting, and brazing requirements call for ventilation where fumes, gases, or dust may create harmful exposure. Fluxes containing fluorides also require warnings about irritating fumes.
Magnesium oxide fume can form when magnesium is burned, welded, or thermally processed. The NIOSH Pocket Guide for magnesium oxide fume identifies inhalation as an occupational exposure concern.
- Clear combustible material, magnesium dust, and loose chips from the hot-work area.
- Provide suitable local exhaust or general ventilation for the process and flux being used.
- Wear appropriate eye protection, heat-resistant gloves, protective clothing, and additional respiratory protection when the hazard assessment requires it.
- Keep the correct Class D extinguishing agent available for magnesium-metal hazards.
- Follow the safety data sheet for the exact flux and filler product rather than assuming all magnesium consumables behave alike.
Note: Structural, aerospace, pressure-containing, or safety-critical magnesium joints should use a qualified brazing procedure developed or approved by personnel familiar with the exact alloy, filler, flux, and service requirements.
What Filler Metals Work Best?
The best filler metal is one whose melting range, chemistry, corrosion behavior, and mechanical properties suit the exact magnesium base alloy. An alloy name alone is not enough to establish compatibility.
A key recognized brazing filler is BMg-1, a magnesium-aluminum-zinc filler associated with AZ92A composition. The current AWS A5.8 specification family covers magnesium filler metals along with other brazing-filler groups.
AZ31 and AZ61 should not be presented as universal brazing fillers simply because they are magnesium alloys. AZ31 is widely encountered as a magnesium base alloy, while AZ61A is also classified and sold for magnesium welding and some joining applications. Filler selection must follow the intended brazing procedure rather than a general AZ-series rule.
Technical literature also describes lower-temperature Mg-Al, Mg-Al-Zn, Mg-In-Zn, and specialized aluminum-containing filler systems. For example, research on AZ31B magnesium brazing demonstrated specially developed flux and filler combinations below 490°C. Those experimental systems should not be treated as interchangeable with qualified commercial BMg fillers.
Aluminum-silicon materials also appear in specialized magnesium joining research, particularly for dissimilar joints and engineered interlayers. They are not a universal substitute for a magnesium brazing filler because intermetallic formation, corrosion, and base-alloy compatibility can change the final joint behavior.
What Flux Should You Use?
Use a flux specifically formulated for magnesium and for the filler-metal temperature range. General-purpose silver-brazing or steel-brazing flux is not automatically suitable because magnesium oxide is unusually stable.
Magnesium brazing fluxes commonly rely on chloride and fluoride salts. AWS FB2-A is a recognized magnesium-brazing flux classification. As one commercial example, Superior No. 21 magnesium brazing flux is rated for 480°C to 620°C (900°F to 1150°F) and is formulated for BMg-1.
The usable flux range must overlap the working range of the filler. A flux that becomes inactive before the filler flows cannot protect the joint properly, while overheating the flux can shorten its useful life and increase residue.
- Match the classification: use a magnesium-specific product approved for the selected process.
- Check the activity range: it must cover the required brazing temperature.
- Apply controlled coverage: coat the surfaces that need protection without packing the joint with excessive flux.
- Keep flux dry: many chloride-based products absorb moisture during storage.
- Plan residue removal: do not leave corrosive flux trapped around the finished joint.
How Do You Prepare Magnesium Parts for Brazing?
Preparation should leave the joint surfaces clean, oxide-controlled, accurately fitted, and ready for immediate fluxing. Grease, oil, dirt, heavy oxide, paint, corrosion products, and embedded contamination can all prevent filler flow.
- Identify the alloy. Confirm that the magnesium grade is suitable for the filler and brazing cycle you plan to use.
- Degrease the surfaces. Remove oil and shop contamination with a cleaner appropriate for the alloy and workplace procedure.
- Remove loose oxide or corrosion. Use the surface-preparation method specified for the job without embedding foreign metal into the magnesium.
- Fit and fixture the joint. Brazing depends on controlled clearance and capillary flow, so poorly fitted parts should not be corrected by simply adding more filler.
- Apply magnesium brazing flux. Cover the intended wetting area evenly and follow the manufacturer’s mixing and application instructions.
- Heat according to the qualified filler/flux cycle. Do not use a universal preheat temperature for every magnesium alloy.
- Feed or position the filler correctly. The workpiece should provide the heat that melts and draws the filler through the joint.
- Cool and remove flux residue. Follow the flux manufacturer’s cleaning instructions before the residue has time to promote corrosion.
A fixed 300°F preheat is not a universal magnesium-brazing requirement. Preheating may be part of a particular torch, furnace, or production procedure, but its temperature must come from the qualified process for the actual components.
What Temperature Is Used for Magnesium Brazing?
There is no single brazing temperature for every magnesium alloy. The correct temperature must melt and flow the filler while staying below the solidus of the base material.
| Reference | Temperature | Why It Matters |
|---|---|---|
| BMg-1 filler | About 1120°F to 1160°F (605°C to 627°C) brazing range | Typical reference range for this filler, not a universal range for every magnesium alloy. |
| Example FB2-A magnesium flux | 900°F to 1150°F (480°C to 620°C) active range | The flux must remain active while the selected filler flows. |
| Pure magnesium melting point | About 1202°F (650°C) | Shows why a blanket 1200°F to 1400°F instruction is unsuitable for magnesium brazing. |
PubChem lists pure magnesium’s melting point at about 650°C (1202°F). Individual magnesium alloys may begin melting below that temperature, so the base-alloy solidus, not the pure-element value, sets the real upper limit.
You also should not heat magnesium to an arbitrary amount such as 200°F above the filler liquidus. BMg-1 itself has a liquidus near 1110°F (599°C), while its commonly published brazing range is only modestly higher. Use the filler manufacturer’s or qualified procedure’s actual working range.
Common Magnesium Brazing Problems and Fixes
Most magnesium brazing problems come from oxide contamination, incorrect filler or flux selection, poor joint fit, insufficient heat, excessive heat, or incomplete post-braze cleaning. The appearance of the joint can often point you toward the cause.
Poor Wetting or Filler That Beads Up
If filler sits on the surface instead of spreading, suspect oxide, dirt, inactive flux, or insufficient joint temperature. Stop adding filler and correct the surface condition or heating problem rather than building a large bead on top.
- Clean the surfaces again if contamination is suspected.
- Verify that the flux is intended for magnesium and has not absorbed excessive moisture.
- Confirm that the filler and flux temperature ranges overlap.
- Heat the assembly evenly enough for the workpiece to melt the filler.
Base Metal Starts to Sag or Melt
Distortion or local melting indicates excessive temperature or poor heat distribution. Magnesium provides much less temperature margin than many steels and copper alloys, so continuing to heat can quickly ruin the part.
Reduce heat input, move the heat source rather than dwelling in one area, and verify the base alloy’s solidus before repeating the procedure.
Porosity or Dirty Joint Lines
Porosity can result from contamination, trapped flux, gases, poor fit, or unsuitable starting material. A porous-looking joint should not be accepted automatically just because filler flowed around the outside.
Inspect the joint after cleaning. For important components, use the inspection method and acceptance criteria required by the applicable brazing procedure or engineering specification.
Corrosion Appears After Brazing
Post-braze corrosion often points to retained flux or an unfavorable filler/base-metal combination. Magnesium is already electrochemically active, and chloride-containing residue can make the problem worse.
Remove flux using the manufacturer’s specified cleaning method, inspect crevices where residue can remain trapped, and apply any required post-braze corrosion protection only after the joint is clean.
The Joint Looks Full but Is Weak
A large external fillet does not prove that filler penetrated the joint. Weak joints can result from poor capillary clearance, incomplete wetting, incompatible filler chemistry, overheating, or lack of bonded area.
Do not compensate by piling on more filler. Correct the fit-up and process variables, then qualify the joint through the inspection or mechanical testing required for the application.
Frequently Asked Questions
What Are the Safety Precautions to Be Taken When Brazing and Soldering?
Brazing and soldering require ventilation, suitable eye and skin protection, fire prevention, clean work areas, and safe handling of heated parts and chemicals. With magnesium, also remove combustible chips and dust and keep an extinguishing agent suitable for the magnesium fire hazard available before heating begins.
What PPE Is Required for Brazing?
Brazing PPE normally includes suitable shaded eye or face protection, heat-resistant gloves, protective clothing, and appropriate footwear. Respiratory protection may also be necessary when ventilation alone cannot control fumes or dust, but respirator selection should follow a workplace hazard assessment and the requirements for the specific flux and material.
What Is Brazing Flux Made Of?
Brazing flux composition depends on the metals and working temperature. General brazing fluxes may contain borates and fluorides, while magnesium brazing uses specialized chloride-fluoride salt systems designed to attack magnesium oxide. The exact product must match the filler and process rather than being chosen from a generic flux description.
What Are Common Brazing Mistakes?
Common brazing mistakes include poor cleaning, incorrect joint clearance, mismatched filler and flux, heating the filler directly instead of the assembly, overheating the base metal, and leaving flux residue behind. On magnesium, these errors are especially serious because oxidation, melting, corrosion, and fire risk can develop quickly.
Can Every Magnesium Alloy Be Brazed?
No, not every magnesium alloy can be brazed with the same filler and temperature cycle. Some alloys have solidus temperatures too low for common commercial magnesium fillers, while others may lose important mechanical properties during heating. Confirm base-alloy brazability and filler compatibility before selecting the process.
Conclusion
Magnesium brazing succeeds when the process stays inside a narrow compatibility and temperature window. Start with the exact base alloy, select a proven magnesium filler and matching flux, prepare the surfaces carefully, heat only to the required working range, and remove flux residue completely. Above all, treat magnesium ignition, dust, and fumes as real hot-work hazards rather than ordinary brazing concerns.
Sources
- American Welding Society — Magnesium and Magnesium Alloys: Magnesium brazing processes, brazability, filler metals, fluxes, preparation, and safe practices.
- American Welding Society — A5 Filler Metals Committee: AWS A5.8 coverage of classified magnesium brazing filler metals.
- Superior Flux — No. 21 Magnesium Brazing Flux: FB2-A classification, 480°C to 620°C active range, BMg-1 compatibility, cleaning, storage, and ventilation guidance.
- PubChem — Magnesium: Pure magnesium melting point of approximately 650°C or 1202°F.
- OSHA — 29 CFR 1910.252: Welding, cutting, brazing, ventilation, fluoride-flux, and worker-protection requirements.
- OSHA — Portable Fire Extinguisher Basics: Class D combustible-metal fire guidance covering magnesium.
- NIOSH — Magnesium Oxide Fume: Occupational exposure information for magnesium oxide fume.
- Japan Welding Society — Development of Flux and Filler Metal for Brazing Magnesium Alloy AZ31B: Research on lower-temperature magnesium filler and flux systems.