
If you are comparing the best welding rods for home repairs, practice, structural mild steel, or fast flat welds, the main challenge is matching the electrode to your machine and joint position.
Forney E6013 is the best overall pick here because its 3/32-inch size runs at 50–70 amps and works on AC or DC in all positions. Forney E7018 is the best value when you need a 5-pound low-hydrogen option for stronger structural work.
We chose these picks using current manufacturer specifications, exact model matching, position and polarity requirements, amperage range, package size, and live availability checks.
Best Welding Rods Compared
| Product | Best for | Positions | Diameter | Amperage | Score |
|---|---|---|---|---|---|
|
Budget
|
Beginners and general-purpose mild steel | All positions | 3/32 in | 50–70 A | 86/100 |
|
Mid-range
|
Low-hydrogen structural work | All positions; avoid vertical-down | 3/32 in | 65–100 A | 91/100 |
|
Premium
|
Fast fill on flat and horizontal joints | Flat and horizontal fillets | 5/32 in | 150–230 A | 84/100 |
Best Welding Rods: Our Top Picks
|
Category |
Product |
Score |
|---|---|---|
|
🎯 Best for Beginners |
86/100 |
|
|
🏆 Best for Structural Welds |
91/100 |
|
|
🚀 Best for Fast Fill |
84/100 |
1. Forney E6013
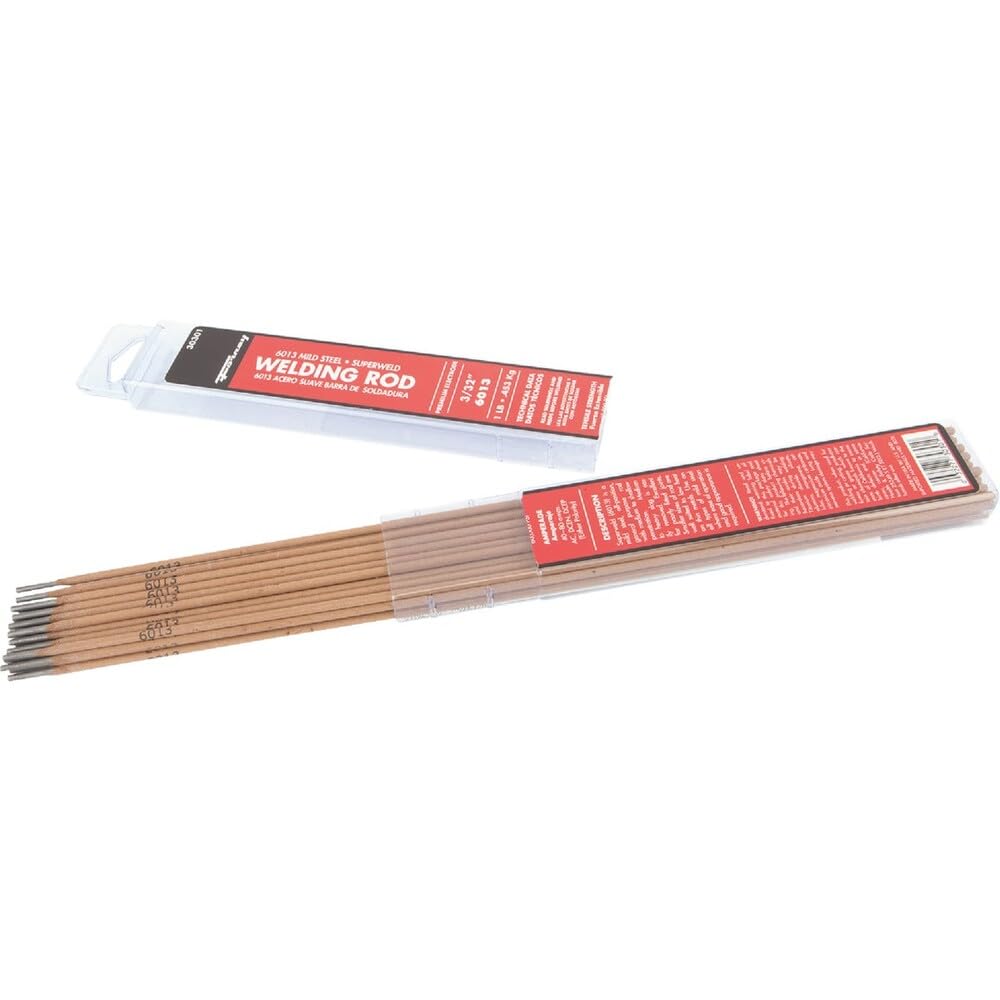
Bottom line: The Forney E6013 is the easiest all-around choice in this lineup for learning, light fabrication, and routine mild-steel repairs. Its low amperage range and all-position rating make it friendly to smaller machines and common shop work.
- Classification: E6013, general-purpose mild-steel stick electrode
- Diameter: 3/32 in, suited to lighter fabrication work
- Package weight: 1 lb, easy for occasional users to store
- Amperage: 50–70 A, manageable for many compact welders
- Polarity: AC, DCEP, or DCEN, broad machine compatibility
Forney E6013 is specified for all-purpose, all-position welding on mild steel. Forney highlights light-gauge metal, sheet metal, duct work, and general fabrication as core uses. The company also lists an 83,000 PSI tensile strength for this exact 30301 model.
The main advantage is ease of operation. Forney describes a steady arc, low spatter, good wetting action, and easy slag removal. Those traits are useful when you are still learning arc length and travel speed or when you want clean-looking results on lighter work.
The trade-off is scope. E6013 is not a low-hydrogen structural electrode, and the one-pound package is aimed more at practice, hobby use, and occasional repair than high-volume fabrication.
|
Pros |
Cons |
|---|---|
|
✅ User-friendly arc and restarts |
❌ Not a low-hydrogen electrode for critical structural work |
|
✅ Good for beginners and general repairs |
❌ Sold in small 1-pound packs may require frequent repurchase |
|
✅ Reliable bead for mild steel |
Situational Benefits
|
Situation |
How It Helps |
|---|---|
|
Learning to Weld |
You get easy arc starts and forgiving behavior when your technique is still inconsistent, which helps you build confidence faster. |
|
Light Repairs |
The rod lays down a consistent bead on typical mild steel repairs, making quick shop fixes straightforward and reliable. |
|
Practice and Skill Building |
Because starts and restarts are predictable, you can practice bead control and travel speed without fighting an unstable arc. |
Using It Well
Start inside Forney’s 50–70 amp range, then fine-tune for your joint and machine. Keep a short, steady arc, clean the joint when practical, and remove slag between passes. Practice on scrap first if the material is thin enough that burn-through is a concern.
2. Forney E7018

Bottom line: The Forney E7018 is the better choice for structural mild-steel work where low-hydrogen performance matters. The five-pound package also gives regular fabricators more electrode per purchase than the one-pound E6013 pack.
- Classification: E7018, low-hydrogen mild-steel electrode
- Diameter: 3/32 in, useful for controlled structural work
- Package weight: 5 lb, practical for repeated shop jobs
- Amperage: 65–100 A, higher demand than E6013
- Polarity: DCEP or DCEN, verify welder compatibility first
Forney positions the Forney E7018 for field erections, steel structures, frames, trailer hitches, chassis, tack welding, and difficult steels. The exact 30705 model is rated at 84,000 PSI tensile strength and 65–100 amps.
The low-hydrogen coating is the reason to choose it over a general-purpose rod when hydrogen control is important. Forney also warns that this model is not recommended for low open-circuit-voltage power sources, so machine compatibility deserves a check before you buy.
One important correction is polarity. Forney’s current page for model 30705 lists DCEP or DCEN. If you rely on AC, look for a rod specifically sold as E7018 AC instead of assuming this package is the AC variant.
|
Pros |
Cons |
|---|---|
|
✅ Low-hydrogen for improved mechanical performance |
❌ Requires dry storage to maintain low-hydrogen properties |
|
✅ Good arc stability and fusion on mild steel |
❌ Less forgiving than ruddle-coated rods for absolute beginners |
|
✅ Pack size reduces frequent repurchasing |
Situational Benefits
|
Situation |
How It Helps |
|---|---|
|
Structural Repairs |
Low-hydrogen deposits resist cracking and yield strong joints for frames, trailers, and load-bearing repairs. |
|
Fabrication Work |
You get consistent fusion and predictable mechanical properties across joints, which simplifies quality control. |
|
Workshop Production |
The five-pound pack keeps you stocked for multiple parts runs and reduces interruptions for restocking. |
Using It Well
Keep low-hydrogen electrodes dry and follow the manufacturer or project procedure after opening. Use the specified 65–100 amp range as your starting window, maintain a short stable arc, and clean slag fully between passes.
3. Blue Demon 7024

Bottom line: The Blue Demon 7024 is the specialist pick for fast metal deposition on flat welds and horizontal fillets. It needs much more amperage than the two 3/32-inch Forney rods and is not meant for vertical or overhead work.
- Classification: E7024, high-deposition carbon-steel electrode
- Diameter: 5/32 in, built for higher deposition work
- Package weight: 5 lb, suited to shop production
- Amperage: 150–230 A, requires a higher-output welder
- Polarity: AC or DCEN, match the machine setup
Welding Material Sales, the manufacturer behind Blue Demon, describes E7024 as a high-speed, heavy iron-powder electrode for high deposition. The classification is limited to flat welding and horizontal fillets, with a 70 ksi minimum tensile strength.
The 5/32-inch size is listed for 150–230 amps. That makes it useful when you want to lay down metal quickly, but it also means a small 120-volt hobby welder may not have enough output for this rod.
This rod makes the most sense for production-style seams, machine bases, truck fabrication, storage tanks, and similar work that can stay in the correct position. For mixed-position field repairs, choose a more position-flexible electrode.
|
Pros |
Cons |
|---|---|
|
✅ Very fast deposition and large smooth beads |
❌ Limited to flat and horizontal positions |
|
✅ Reliable penetration on dirty or rusty steel |
❌ Requires higher amperage; not ideal for small, low-power machines |
|
✅ Compatible with AC and DC power |
❌ Flux load means fewer rods per pound compared with some other types |
Situational Benefits
|
Situation |
How It Helps |
|---|---|
|
Production Runs |
High deposition speed lets you complete repetitive flat seams faster, shortening cycle time for parts runs. |
|
Repair Caps |
You can quickly build up material and produce a smooth cap that requires minimal grinding. |
|
Dirty or Rusty Steel |
The rod tolerates less-than-perfect surfaces and still achieves good penetration and fusion. |
Using It Well
Confirm that your welder can supply the required current before buying. Keep the work in flat or horizontal-fillet positions, start within the manufacturer’s amperage window, and clean the joint rather than relying on the electrode to compensate for contamination.
Forney E6013 vs Forney E7018: Is the Upgrade Worth It?
The E6013 is easier to pair with small welders and general repair work, while the E7018 trades some simplicity for low-hydrogen performance and a larger five-pound package.
- Power demand: E6013 runs at 50–70 A; E7018 runs at 65–100 A.
- Primary job: E6013 favors light general fabrication; E7018 targets structural and low-hydrogen work.
- Polarity: E6013 supports AC, DCEP, and DCEN; the current 30705 page lists DCEP or DCEN.
- Package size: E6013 comes here in 1 lb; E7018 comes in 5 lb.
Which Welding Rod Should You Buy?
- Learning stick welding: get the Forney E6013.
- Light mild-steel repair: get the Forney E6013.
- Low-hydrogen structural work: get the Forney E7018.
- Repeated structural shop jobs: get the Forney E7018.
- Fast flat or horizontal fill: get the Blue Demon 7024.
How We Chose
- Exact model match: we checked the linked model, size, and package against current manufacturer or major-retailer data.
- Machine fit: amperage and polarity were prioritized because they determine whether your welder can run the rod properly.
- Position capability: all-position rods were separated from flat-and-horizontal-only electrodes.
- Job fit: general repair, low-hydrogen structural work, and high-deposition production were treated as different needs.
- Safety and freshness: we checked current product documentation and recall search results before keeping each recommendation.
How to Use and Store Stick Electrodes
Start With the Manufacturer Amperage Range
Use the specified current range as your starting point, then fine-tune for joint type, material thickness, arc behavior, and your machine. A rod that is too large for the available current will be frustrating to start and may not run correctly.
Keep the Arc and Travel Consistent
Use a short, controlled arc and a steady travel speed. Remove slag between passes, and practice on scrap before a critical repair. Joint cleanliness still matters even when an electrode is described as forgiving.
Keep Electrodes Dry
Store all electrodes away from moisture. Low-hydrogen E7018 needs stricter handling when weld quality requirements depend on hydrogen control, so follow the manufacturer and any applicable welding procedure after opening the package.
Use Proper Welding Safety
Wear a suitable welding helmet, gloves, protective clothing, and eye protection. Ventilate the work area, manage fumes, keep flammables away, and handle hot metal and slag as burn hazards.
Welding Rod Buying Guide
Match the AWS Classification to the Job
E6013 is the general-purpose choice here, E7018 is the low-hydrogen structural option, and E7024 is the high-deposition specialist. If you want one forgiving rod for light work, Forney E6013 is the natural fit.
Check Welding Position Before Anything Else
Position is a hard limit. The Forney E6013 and E7018 choices offer broad position capability, while E7024 is limited to flat welds and horizontal fillets. For mixed-position jobs, do not choose Blue Demon 7024 just for its deposition speed.
Match Amperage to Your Welder
The three rods here span very different power needs. E6013 uses 50–70 amps, E7018 uses 65–100 amps, and the 5/32-inch E7024 uses 150–230 amps. Check your machine’s actual output range before ordering.
Confirm Polarity
Polarity can change by classification and exact product. The E6013 supports AC, DCEP, and DCEN. The current Forney 30705 E7018 page lists DCEP or DCEN, while the E7024 manufacturer data lists AC or DCEN. When in doubt, match the package and manufacturer sheet to your welder.
Choose Package Size for How Often You Weld
A one-pound pack is convenient for occasional repairs and practice. Five-pound packs suit regular shop use and reduce how often you reorder, but only if you can store the electrodes properly and actually use that classification often.
Mistakes to Avoid When Buying Welding Rods
- Buying by strength alone: position, polarity, and machine output can matter more.
- Assuming all E7018 is AC-ready: verify the exact variant and current manufacturer data.
- Oversizing the electrode: make sure your welder can supply the needed amperage.
- Ignoring storage: keep electrodes dry, especially low-hydrogen rods.
- Using E7024 out of position: reserve it for flat and horizontal-fillet work.
FAQs
Which welding rod is easiest for beginners?
For this lineup, the Forney E6013 is the easiest starting point. Forney describes it as a general-purpose, all-position electrode for mild steel with easy operation, low spatter, and a steady arc. The 3/32-inch rod runs at 50–70 amps, which also makes it easier to pair with many smaller stick welders used for practice and light repair.
Can E6013 weld in all positions?
Yes. Forney lists the 30301 E6013 as an all-position electrode for mild steel. It is especially useful where easy operation and bead appearance matter, including light-gauge fabrication. Position capability does not remove the need for good joint preparation, correct amperage, a short stable arc, and the right travel angle for the joint you are welding.
Is the Forney 30705 E7018 an AC welding rod?
The current Forney product page for model 30705 lists DCEP or DCEN polarity, not AC. That matters because E7018 and E7018 AC are different product variants. If your machine is AC-only, confirm compatibility before buying and consider an electrode specifically labeled E7018 AC rather than assuming every E7018 package will run correctly on your welder.
What is E7024 best used for?
E7024 is built for high deposition on flat welds and horizontal fillets. Welding Material Sales lists the classification for flat and horizontal-fillet positions, with the 5/32-inch size running at 150–230 amps. It is a strong choice for fast fill and production-style work when the joint can stay in the proper position and the machine has enough output.
Can I use E7024 for vertical or overhead welding?
No. E7024 is not an all-position electrode. The manufacturer data lists it for flat welds and horizontal fillets, so vertical and overhead work call for a different classification. If you need more positional flexibility, the E6013 and E7018 choices in this guide are better fits, provided their other material and machine requirements match your job.
How should I store E7018 welding rods?
Keep E7018 electrodes dry and follow the manufacturer or applicable welding procedure for storage after opening. Moisture control matters more with low-hydrogen electrodes because their purpose is to limit hydrogen in the weld deposit. For code or critical structural work, follow the project specification and electrode-handling rules rather than relying on casual shop storage alone.
How do I choose between a 3/32-inch and 5/32-inch welding rod?
Start with your welder’s output and the job size. The 3/32-inch Forney rods here run at 50–70 amps for E6013 and 65–100 amps for E7018. The 5/32-inch Blue Demon E7024 requires far more current at 150–230 amps. Larger electrodes suit higher deposition work but can overwhelm small machines and thin material.
Customer Preferences
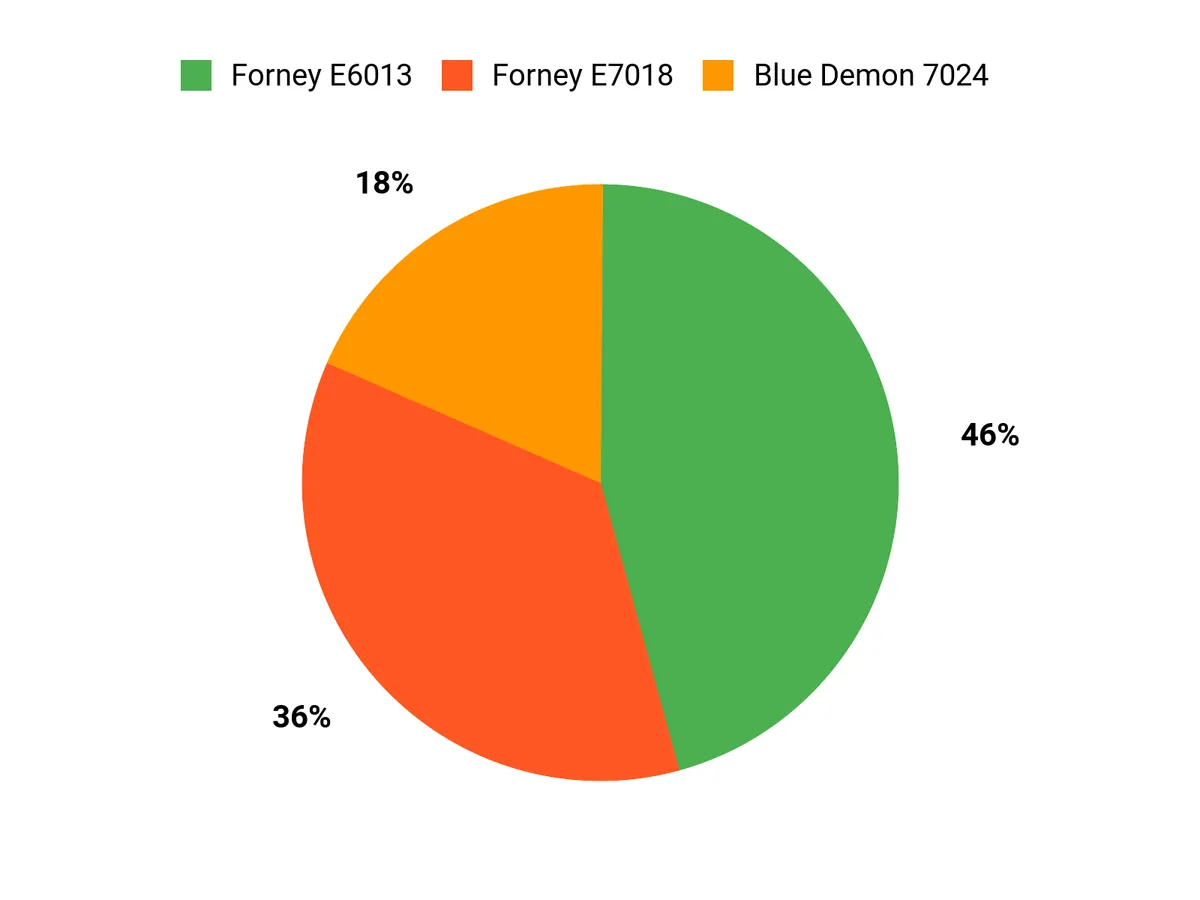
Preference usually follows the job. E6013 suits welders who prioritize easy operation and lower current, E7018 suits low-hydrogen structural work, and E7024 suits fast deposition in flat and horizontal positions. Match the rod to your machine and joint instead of expecting one electrode to cover every task.
Final Verdict
Among these best welding rods, the Forney E6013 is the most flexible starting point for beginners and general mild-steel repairs. The Forney E7018 is the stronger fit for low-hydrogen structural work, while the Blue Demon 7024 is the specialist for high-deposition flat welding.
For a larger low-hydrogen package, compare the Forney E7018. For fast flat and horizontal fill, see the Blue Demon 7024.
| Forney 30301 E6013 Welding Rod, 3/32-Inch, 1-Pound | Forney 30705 E7018 Welding Rod, 3/32-Inch, 5-Pound | High Speed, Carbon Stl Electrode, 5/32, 5lb | |
|---|---|---|---|
|
|
|
|
|
| Rating | 4.6/5 (6,944 reviews) | 4.5/5 (2,184 reviews) | 4.6/5 (123 reviews) |
| Material | Mild Steel | Mild Steel | Steel |
| Item Weight | 1 pound | 5.2 pounds | 5.2 pounds |
| Dimensions | 0.75 x 1.63 x 15.25 inches | 14.63 x 3.5 x 1.75 inches | 16 x 3 x 3 inches |
| Shop Now | Shop Now | Shop Now |
[…] dependence on opaque labels or tradition. Additionally, understanding these codes can enhance long-term savings and durability, ensuring weld integrity over […]
[…] weld process greater freedom from avoidable defects. Additionally, understanding the importance of low-hydrogen characteristics can enhance the overall quality of your […]
[…] A flush contour symbol, also above or below, indicates surface requirements for a liberated, finished joint. These symbols provide precise, compact instruction for fabrication, inspection, and disciplined weld execution, ensuring consistency in results for common welding tasks. […]
[…] from uncertainty, replacing assumption with measurable evidence, particularly in contexts where low-hydrogen properties are critical to weld […]
[…] structural welding applications with low-hydrogen characteristics. Additionally, understanding the selection criteria for welding rods can help users make informed choices based on their specific […]
[…] best all-around welding rods are therefore not simply the rods with the “strongest” flux. The correct electrode is the one […]
[…] and welder technique. Electrode selection also matters for applicable processes; this guide to all-around welding rods explains common electrode choices for general […]
[…] type gives the welder more control, more reliability, and more durable results. Additionally, using low-hydrogen rods can significantly enhance the strength and integrity of your welds, especially in critical […]
[…] heat input and cooling are carefully governed for liberation from failure. Additionally, utilizing low-hydrogen rods minimizes the risk of cracking during the welding […]
[…] work, more durable fabrication, and greater control over industrial conditions. Understanding the mechanical properties of metals enhances the ability to make informed decisions during welding […]
[…] work, because the process is visually evaluable and comparatively easy to learn. Additionally, long-term savings can be realized through the efficient and durable bonds formed using this […]
[…] seeking durability without dependence on wasteful material cycles. Additionally, understanding welding rod selection criteria can enhance the effectiveness of using ferrous metals in various […]
[…] because control of stress is the primary defense against crack propagation. Additionally, using low-hydrogen rods during the repair process can significantly reduce the risk of cracking in cast […]
[…] you also use stick welding, this guide to general-purpose welding rods covers other electrode types. Low-hydrogen stick-electrode classifications should not be used as […]
[…] Full penetration should therefore not be treated as the default for every butt weld. It may be necessary in critical pipe, pressure, or structural joints, while other applications are designed around PJP welds. Electrode or filler selection also matters, especially where a procedure calls for controlled hydrogen levels; see this overview of general-purpose welding rods and low-hydrogen options. […]
[…] the code also makes it easier to match a consumable to common welding applications instead of choosing by wire diameter […]
[…] to the material and service requirements instead of choosing only by ease of use. This overview of all-around welding rods can help explain the broader differences between electrode […]
[…] soft, clean, structurally compatible materials over hardened alternatives. Additionally, using low-hydrogen rods in welding processes can enhance the overall integrity of the bond by minimizing cracking […]